THE LEADING TECHNOLOGY COMPANY
Clean Exhaust Gas.
Recovering Energy.
Transforming Industry.
Ceram Austria develops and produces ceramic
high-performance technologies for exhaust gas purification,
heat storage, and decarbonization.
Used worldwide – since 1921.
TECHNOLOGIES
Technical excellence that delivers economic value.
Our high-performance ceramic products are deployed worldwide in emission control, heat storage, and decarbonization and are industry-leading.
Emission Control
Heat Storage
Decarbonization
WHY CERAM AUSTRIA
Technology Excellence. Application Intelligence. Production Competence.
Our products succeed worldwide because we precisely design each solution to meet the requirements of each specific plant. For us, technology excellence means the consistent optimization of performance, robustness, and economic efficiency for every application.
reference plants in demanding industrial processes worldwide
production capacity at our Frauental, Styria location
customers worldwide who trust CATLife™ Services
installed peak power capacity with Ceram SCR catalysts
gas turbine and gas engine applications on all continents
APPLICATION FIELDS
Proven in Practice.
From power generation to process industries and mobile applications at sea and on land, Ceram Austria delivers industry-leading solutions for emission control and energy efficiency in industries where reliability and precision are critical. Our ceramic catalysts and heat storage systems are deployed worldwide and have proven themselves in over 200 international projects under real and often extreme operating conditions.
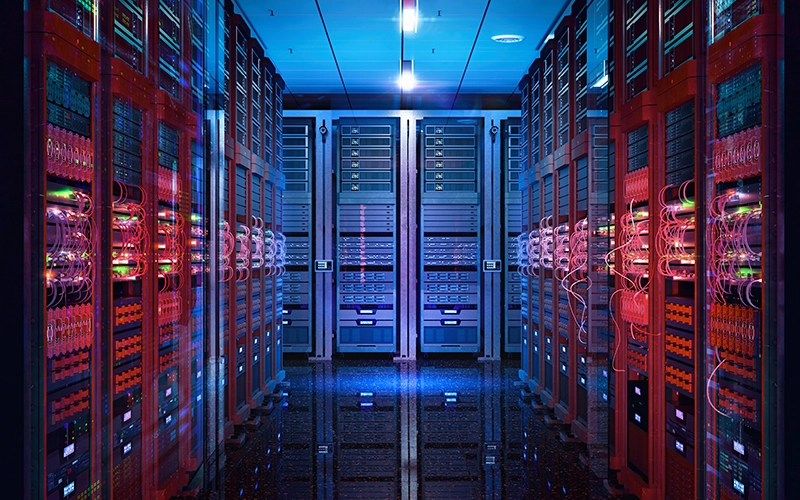
POWER GENERATION
The catalyst behind data center computing power
Our catalysts are the proven solution for reliable power supply to data centers using gas turbines and gas engines. Our products are the foundation for reliable compliance with statutory emission regulations and thus for operating permits. Ceram catalysts ensure highly efficient, long-lasting, and economically optimal operation of gas engine and gas turbine plants in over 200 international projects. Especially in emergency power supply for data centers, where short response times and absolute operational reliability are top priorities, our solutions stand out for their robustness against changing load profiles and increasing emission requirements.
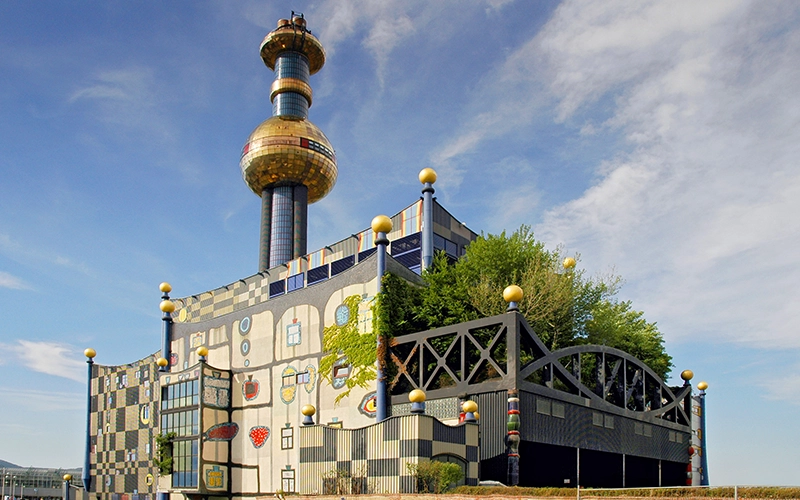
WASTE INCINERATION & BIOMASS
High performance under difficult exhaust gas conditions
Our SCR catalysts for biomass and waste incineration plants are optimized for high conversion rates at low and varying temperature conditions and exhaust gas compositions. Ceram has an extensive track record in the thermal treatment of municipal solid waste, hazardous and medical waste, refuse-derived fuels (RDF), and waste-derived biomass. Our catalysts reduce NOx at low temperatures and reliably break down dioxins and furans. By deploying our solutions, plant operators permanently comply with the strictest emission limits even with fluctuating fuel compositions. As market leaders, we set the standards worldwide for the best value for money in the industry.
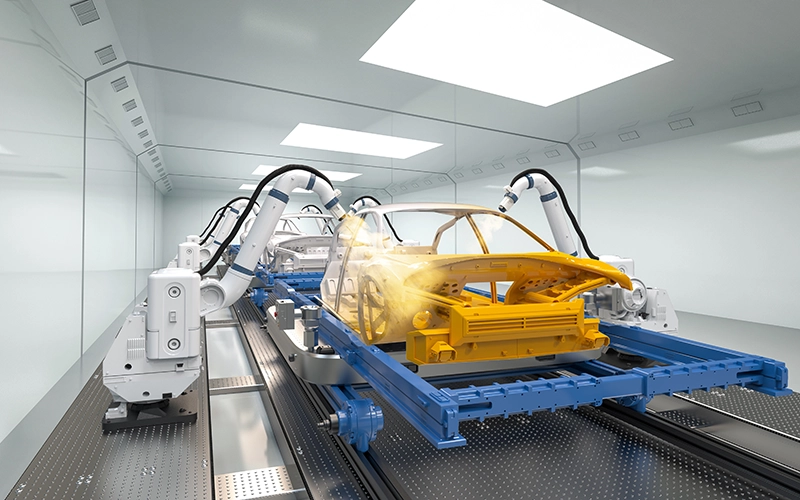
PROCESS INDUSTRY
Heat storage solution for efficient RTOs
Ceram has been developing and manufacturing high-quality ceramic heat storage systems for RTO plants for more than 20 years, in which harmful volatile organic compounds (VOCs) are thermally destroyed. Thermal oxidation operates at high efficiency, ideally without the use of auxiliary fuel. Our honeycomb technology is based on decades of materials research and production experience. From the cement industry to coating and painting plants to the semiconductor and chemical industries, we deliver the right heat storage systems for every application. Operators benefit from our experience in engineering, delivery, and service for virtually any plant size.
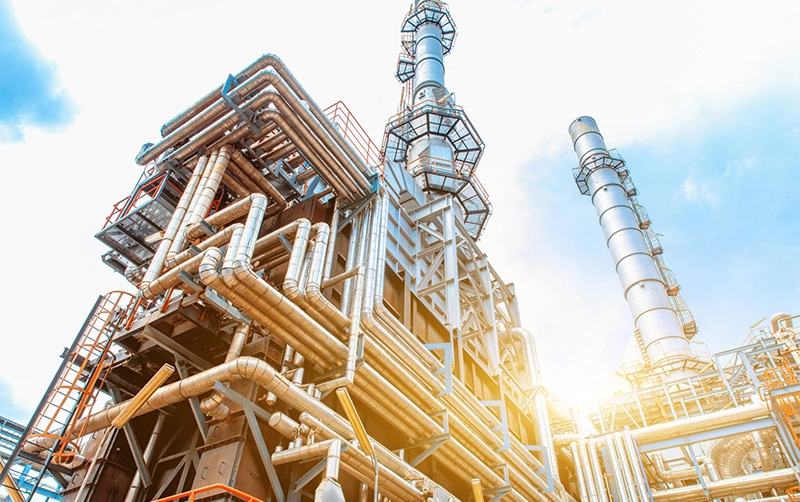
CHEMISTRY & PETROCHEMISTRY
Uncompromising reliability in operation
Conditions for chemical and petrochemical processes are rarely constant and demand uncompromising performance over the entire catalyst lifespan. Unplanned disruptions or shutdowns are not an option, which is why customers trust the robustness and quality of Ceram catalysts. In FCC units, ethylene crackers, and refinery processes, temperature and pollutant profiles can change according to operating parameters. Our catalysts are engineered to ensure stable conversion rates, proven long-term stability, and permanent compliance with strict emission limits even under these variable conditions.
MOBILE APPLICATIONS
Reliable under changing conditions and limited installation space
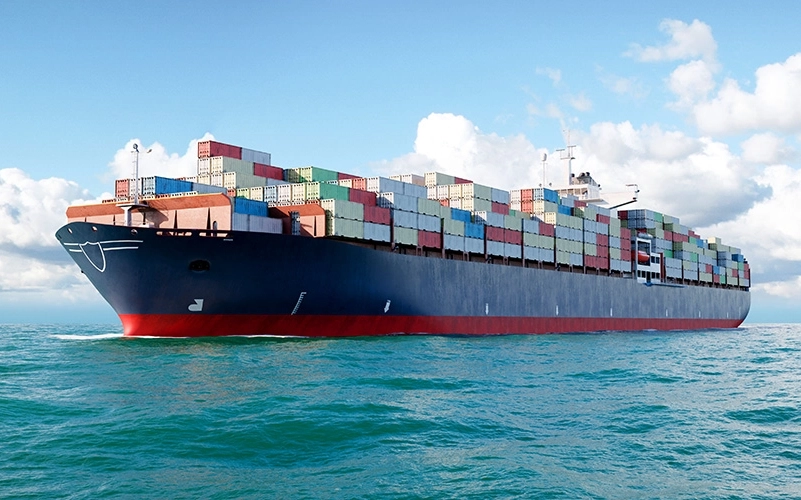
Engines operate under changing operating conditions and installation space for marine and mobile applications is usually limited. Ceram's SCR and ASC (Ammonia Slip Catalyst) solutions enable compliance with strict emission limits for ships, off-road, and stationary engines (IMO Tier III and EU STAGE V) while ensuring long service life. Our product portfolio for round catalysts is used for diesel and gas engines and will increasingly be deployed for alternative fuels in the future. As a long-standing development partner, we support manufacturers and operators from technical engineering through certification to ongoing operation.
Catalyst management over the entire product lifecycle
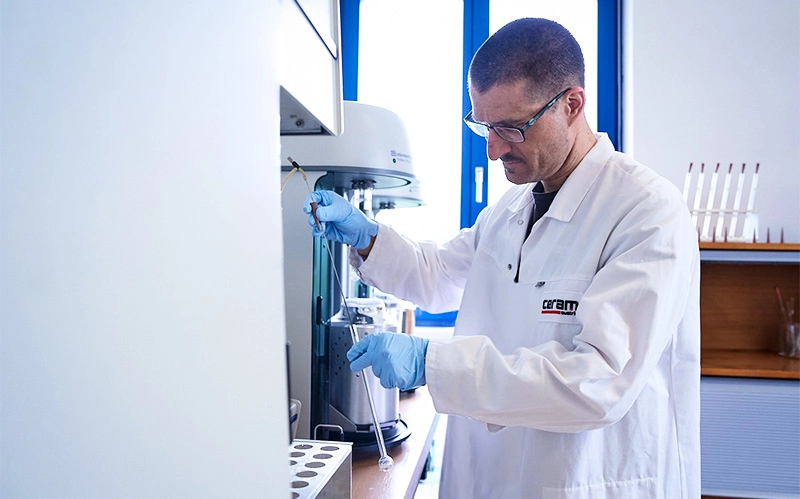
Catalyst management services are a core component of our business. We leverage our expertise in catalyst implementation and the knowledge from our catalyst laboratory to offer the most comprehensive catalyst management service package in the industry. Our CATLife® team of engineers brings years of practical experience and industry knowledge to our service program. Our global presence and the diversity of our application experience give us a unique and comprehensive perspective in catalyst management. From sampling and laboratory analysis to reactivation and replacement, we ensure that plants comply with applicable emission regulations at all times.
CORPORATE FILM
We live technology. We think environment.
Behind every catalyst, every heat storage system, and every solution are people who understand research,
production, and service as a calling. For over 100 years, we have been improving global pollutant and CO₂ balances together with
our partners. Driven by passion for a
clean environment and awareness of our responsibility to future generations,
we continue our success story.
High-performance ceramic technologies for exhaust gas cleaning, heat storage, and decarbonization.
Expertise in ceramic processing since 1921.
Gamserstraße 38 · 8523 Frauental a. d. Laßnitz
office@ceram-austria.com · +43 3462 2000-0
TERMS AND CONDITIONS
CERTIFICATIONS
ISO 9001
ISO 14001
ISO 45001
ISO 50001
ISO 3834-2